

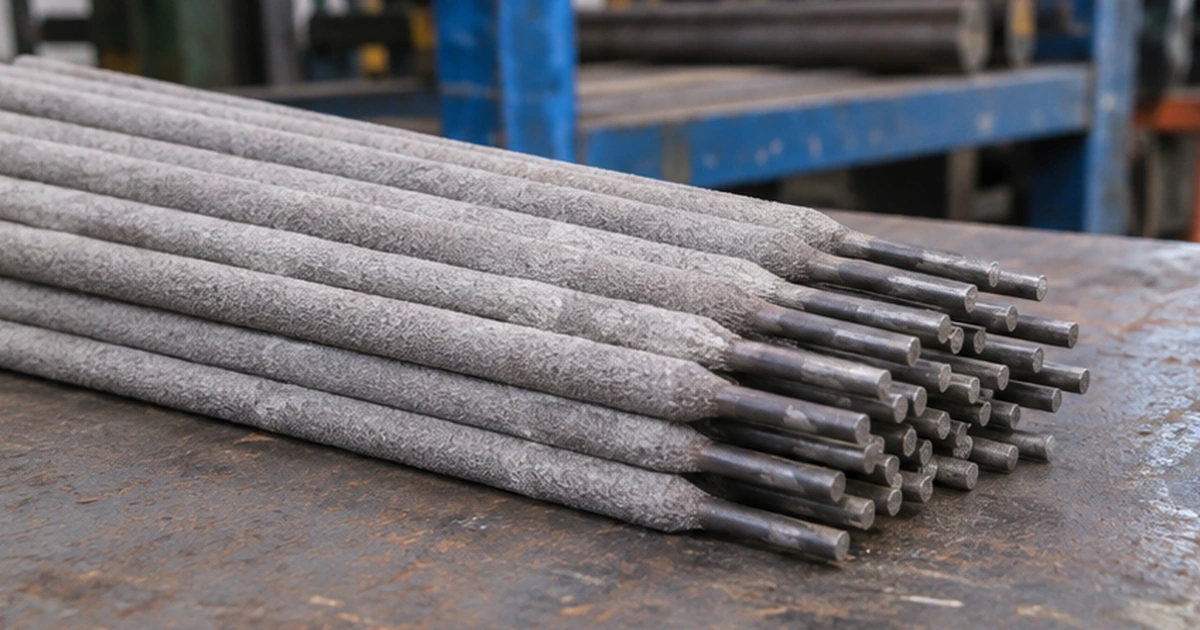
What Is Ferrocito 180, an E7024 Electrode
Ferrocito 180 is a rutile E7024 electrode with iron powder in the coating. It has a recovery of about 180%, which means it deposits roughly twice as much metal per electrode as a standard rutile type. It is made for fast, economical fillet welds and for filling passes.
It can be run in drag (contact) technique with the tip touching the parent metal, and the slag lifts off easily. TWI explains the different coating types in its guide to manual metal arc welding.
Classification
- AWS A5.1: E7024
- ISO 2560 (former edition): E 51 3 RR 180 42
- DIN 1913 (withdrawn): E 51 32 RR 11 180
Base Materials
- Non-alloy structural steels St 33 to St 52 (today S235 to S355 under EN 10025)
- Fine-grain steels StE 26 to StE 36
- Boiler plate HI, HII, HIII and 17Mn4
- Shipbuilding steels, grades A, B, C and D
- Cast steels GS 38, GS 45 and GS 52
Typical Weld Metal Data
Chemical composition (typical, %)
- C 0.08
- Mn 0.80
- Si 0.35
Mechanical properties (all-weld metal)
- Tensile strength: 510–610 N/mm²
- Yield strength: above 380 N/mm²
- Elongation (L = 5d): above 24%
- Charpy V impact at +20 °C: above 60 J
Current and Positions
AC or DC with the electrode negative. Typical ranges:
- Ø3.2 × 450 mm: 120–180 A
- Ø4.0 × 450 mm: 180–220 A
- Ø5.0 × 450 mm: 260–310 A
Positions: flat, and horizontal fillet welds. Like all E7024 electrodes, it is not used for vertical or overhead work.
Where E7024 Makes Sense
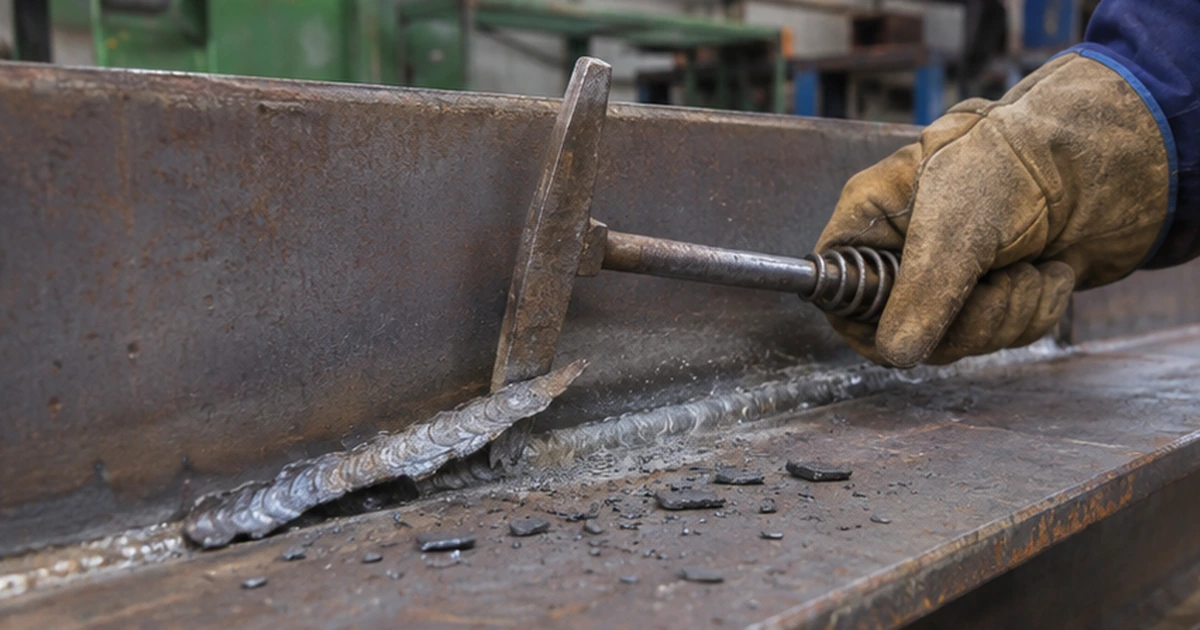
E7024 electrodes are used for long, repetitive fillet welds in the flat and horizontal positions: beams, stiffeners, brackets and panel work in shipyards and steel fabrication shops. On these joints, the high deposition rate cuts welding time and electrode changes.
Technique
- Drag the electrode lightly on the joint at about 45° to both plates
- Do not weave: run straight stringer beads
- Keep a steady travel speed to control bead size
- Let the slag cool before removing it
Limits
E7024 is not a low-hydrogen electrode and AWS A5.1 does not require impact testing for it. For joints with toughness requirements at low temperature, for thick restrained sections or for vertical and overhead welding, a basic E7018 type is used instead.
Fillet Size
Because E7024 deposits so much metal, it is easy to make fillets larger than the drawing asks for. Oversized fillets add cost, weight and distortion without adding useful strength, so travel speed should be set to give the specified leg length and checked with a fillet gauge.
From My Experience
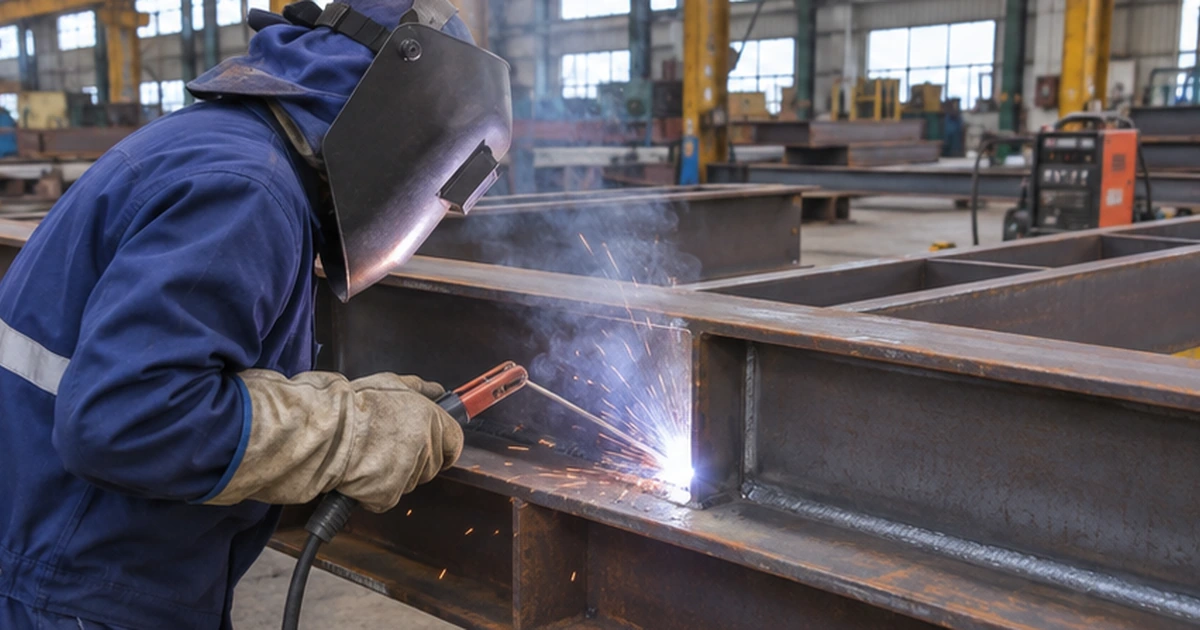
In fabrication shops, an E7024 is what I reach for on long horizontal fillets where nothing more than strength at room temperature is required. As soon as the drawing shows impact values or the joint goes vertical, I change to a basic electrode.
Conclusion
Ferrocito 180 is a high-recovery E7024 electrode for flat and horizontal fillets on structural, boiler and ship steels, where speed and low cost per metre matter. For other electrode types, see steel welding electrodes. Confirm data on the latest manufacturer datasheet before use.
If you found this article useful, feel free to share it with colleagues who work with fillet welding. — Zisis
Need Help on a Project?
For MMA/SMAW welding on marine and industrial work, see MMA/SMAW Welding or request a quote.